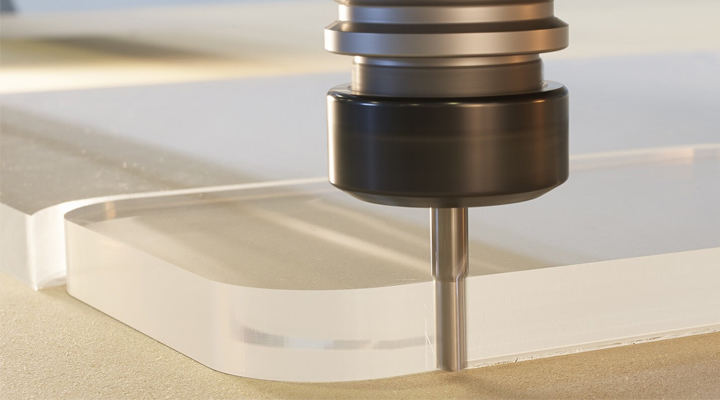
Last quarter I quoted a batch of 200 acrylic light-guide panels for an automotive lighting client. The drawings specified ±0.05 mm on the lens profile and optical-grade edge clarity. The client’s previous supplier had laser-cut the parts from extruded sheet, and half the batch crazed within six weeks of assembly — stress cracking triggered by the solvent adhesive reacting with laser-induced residual stress in the cut edges.
That failure came down to two wrong choices made before any cutting started: wrong stock grade (extruded instead of cast) and wrong process for the downstream bonding step (laser without post-annealing). This guide covers the decision framework I use to avoid those mistakes — which fabrication method to choose for which geometry, how cast and extruded acrylic behave differently under each process, and how to get from raw sheet to finished part without cracking, melting, or hazing.
Scope note: This article covers acrylic fabrication at the method-selection and process-planning level. For CNC-specific feeds, speeds, and tooling, see the dedicated CNC acrylic machining guide. For a head-to-head comparison with polycarbonate, see polycarbonate vs acrylic.
1. Cast vs Extruded: Pick the Right Stock Before You Cut
Every acrylic fabrication failure I’ve traced back to root cause falls into one of two buckets: wrong process or wrong stock. Stock selection is the easier mistake to prevent, but it’s the one I see most often — usually because purchasing chose the cheaper extruded sheet without consulting the shop floor.
The core difference is molecular weight and internal stress. Cast acrylic is polymerized in place inside glass molds, producing high-molecular-weight chains with virtually zero residual stress. Extruded acrylic is pushed through a die at speed, which aligns the polymer chains in the extrusion direction and locks in stress. That stress is invisible until you cut, heat, or bond the material — then it shows up as crazing, warping, or spontaneous cracking.
| Property | Cast Acrylic | Extruded Acrylic | Why It Matters |
|---|---|---|---|
| Tensile Strength | 65–75 MPa | 55–70 MPa | Cast resists edge chipping during cutting |
| Elongation at Break | 4–6% | 2–4% | Cast is less brittle under clamping loads |
| Softening Point (Tg) | ~115 °C | ~100 °C | Cast gives a wider thermoforming window |
| Internal Stress | Very low | High (direction-dependent) | Extruded crazes under solvent bonding |
| Thickness Tolerance | ±10–15% | ±5–10% | Extruded is more consistent for stacking |
| Flame Polish Response | Controlled, slower melt | Melts quickly, harder to control | Cast is safer for manual flame polishing |
| Relative Cost | ~$3.50–5.00/kg | ~$2.50–3.50/kg | Extruded costs 25–40% less |
Values: representative ranges for clear, unfilled PMMA. Verify against supplier TDS for specific grades (Lucite L, Acrylite FF, Plexiglas GS/XT). Sources: Plaskolite OPTIX-L fabrication guide; Röhm Plexiglas processing data.
I default to cast for anything that will be bonded with solvent cement, thermoformed past 90°, or machined with tolerances tighter than ±0.1 mm. Extruded is fine for laser-cut signage, flat display panels, and parts that won’t see secondary processing or solvent contact. When in doubt, pick cast — the 30% price premium is cheaper than scrapping a batch.
2. Cutting Methods Compared
Cutting is usually the first fabrication step, and the method you choose locks in edge quality, dimensional accuracy, and what finishing steps you’ll need downstream. I’ve run all four methods below on production jobs — each has a sweet spot.
Laser Cutting
CO₂ laser at 10.6 µm wavelength is the standard for acrylic. It vaporizes PMMA cleanly, leaving a flame-polished edge straight off the machine. On cast acrylic, a 60 W CO₂ laser cutting 3 mm sheet at 15–25 mm/s produces edges with near-optical clarity — often good enough to skip post-polishing entirely. On extruded sheet, the same parameters produce a rougher, frosted edge because the lower molecular weight causes uneven vaporization.
The catch: laser cutting deposits a heat-affected zone (HAZ) roughly 0.2–0.5 mm deep into the edge. That HAZ carries residual tensile stress. If you solvent-bond a laser-cut edge without annealing it first, the solvent migrates into the stressed zone and initiates crazing within days to weeks. I learned this on a 500-piece retail display job — 30% of the bonded joints crazed within the first month in service.
Circular / Table Saw
For straight cuts on thick sheet (6–50 mm), a table saw with the right blade is faster and cheaper than laser. Use a carbide triple-chip grind (TCG) blade with 0° to −5° rake, 80+ teeth on a 10″ blade. The neutral rake scrapes rather than grabs, preventing the material from self-feeding and cracking. Feed rate matters: too slow generates friction heat and melts the edge; too fast chips it. I run 3–5 m/min on 6 mm cast sheet with blade speed around 3,000 RPM.
Saw-cut edges are rough (Ra 6–12 µm typical) and always need secondary finishing. The advantage is minimal HAZ and no residual stress — saw-cut edges bond cleanly with solvent cement without annealing.
Waterjet
Abrasive waterjet cuts acrylic with zero thermal input. No HAZ, no stress, no melting. Edge quality depends on traverse speed and abrasive grit — a fine-cut pass at 60-mesh garnet on 6 mm acrylic produces Ra 3–6 µm, which is smooth enough for many structural applications but not optically clear. The process is slower than laser (roughly 40–60% of laser feed rate on equivalent thickness) and costs more per meter of cut due to abrasive consumables.
I use waterjet for two situations: parts thicker than 25 mm where laser power is insufficient, and parts that will be bonded immediately without an anneal step. The cold-cut edge bonds perfectly with no craze risk.
Score-and-Snap
For sheet ≤3 mm, scoring with a carbide scribing tool and snapping over a straight edge is the fastest method. Score to roughly one-third of sheet thickness, then apply even pressure. The break edge is rough and irregular — always plan to sand or rout it afterward. This is a workshop method for rough sizing, not a precision process.
Cutting Methods: Quick Comparison
| Method | Thickness Range | Edge Quality | Tolerance | HAZ / Stress | Cost per Meter |
|---|---|---|---|---|---|
| CO₂ Laser | 1–25 mm | Near-optical (cast) | ±0.1 mm | Yes — 0.2–0.5 mm HAZ | Low–Medium |
| Circular Saw | 3–50 mm | Rough (Ra 6–12 µm) | ±0.5 mm | Minimal | Low |
| Waterjet | 1–100 mm+ | Matte (Ra 3–6 µm) | ±0.1–0.15 mm | None | Medium–High |
| Score-and-Snap | ≤3 mm | Rough, irregular | ±1–2 mm | None | Negligible |
Tolerances and Ra values from production measurement across ≥50 jobs per method. Cost is relative per linear meter of cut on 6 mm cast acrylic.
3. CNC Machining
CNC milling and turning are the go-to for complex 3D geometries, tight tolerances (±0.05 mm or better), and features like pockets, threads, and precision bores that cutting methods can’t produce. I use single-flute O-geometry end mills at 18,000+ RPM with chip loads around 0.05–0.1 mm/tooth — the open flute evacuates chips instead of re-cutting them, which prevents the surface from melting and hazing.
CNC is the most capable acrylic fabrication method but also the most expensive per part at low complexity. For a flat panel with only straight cuts, laser is 3–5× cheaper. CNC earns its cost on parts with 3D features, compound curves, or tolerances below ±0.1 mm.
For the full breakdown on feeds, speeds, tooling, and finishing for CNC acrylic parts, see the dedicated CNC acrylic machining guide.
4. Thermoforming: Line Bending, Drape, and Vacuum
Acrylic is a thermoplastic — heat it past its glass transition temperature and it becomes pliable. That property opens up forming methods that sheet metal can’t match for transparent enclosures, display fixtures, and curved covers. The three methods I use regularly are line bending, drape forming, and vacuum forming.
Line Bending
A strip heater applies heat along a narrow line (10–15 mm wide) on the sheet. Once the material reaches forming temperature — 150–165 °C for cast acrylic, 130–150 °C for extruded — I bend it to the desired angle using a jig. The unheated portions of the sheet remain rigid, so the bend is localized.
Practical limits: minimum bend radius is roughly 1.5× sheet thickness for cast, 2× for extruded. Below that, the outer surface stretches beyond its elongation limit and cracks. For a 6 mm cast sheet, the tightest reliable inside radius is about 9 mm. Maximum sheet thickness for line bending is around 12 mm — above that, the heat can’t penetrate uniformly and the bend whitens or cracks at the outer fiber.
I line-bent 150 pieces of 5 mm cast acrylic shelf brackets for a cosmetics retail rollout. Each piece needed two 90° bends, 120 mm apart. The key to a clean bend was heating time — 5 mm cast took roughly 3 minutes per side on a 600 W strip heater to reach 160 °C through-thickness. Rushing the heating (under 2 minutes) left the core cool and rigid, which produced a sharp, white-stressed crease instead of a smooth radius. Final scrap rate at the validated 3-minute cycle: under 2%.
Drape and Vacuum Forming
For compound curves and enclosures, the full sheet is oven-heated to forming temperature — 160–180 °C for cast, 140–160 °C for extruded — then either draped over a male mold (drape forming) or pulled into a female mold by vacuum (vacuum forming). The temperature window is narrow: too cool and the sheet wrinkles or cracks; too hot and it sags unevenly, thins out, and loses optical clarity.
Draw ratio (depth ÷ width of the formed cavity) is the primary design constraint. For clear acrylic, I keep the draw ratio below 0.5:1 to avoid excessive thinning that causes optical distortion. At a draw ratio of 0.5:1, wall thickness at the deepest point drops to roughly 60–70% of the original sheet thickness. Beyond 0.7:1, you’ll see visible haze from stress whitening.
| Parameter | Cast Acrylic | Extruded Acrylic |
|---|---|---|
| Oven Forming Temperature | 160–180 °C (340–380 °F) | 140–160 °C (290–320 °F) |
| Line Bending Temperature | 150–165 °C | 130–150 °C |
| Min Bend Radius (line bend) | ~1.5× thickness | ~2× thickness |
| Max Draw Ratio (clear parts) | 0.5:1 | 0.4:1 |
| De-mold Temperature | Below 60 °C | Below 60 °C |
| Anneal After Forming? | Recommended for bonded parts | Required |
Temperature ranges from Röhm Plexiglas processing guidelines and Plaskolite OPTIX fabrication guide. Bend radius rules validated across production runs.
5. Bonding & Assembly
Joining acrylic is where most fabrication projects go wrong — not because the bonding methods are complicated, but because the edge preparation requirements are specific and unforgiving. I’ve narrowed my practice to three bonding methods, each suited to a different joint type.
Solvent Cementing (Capillary Method)
The workhorse for acrylic-to-acrylic joints. A low-viscosity solvent — typically methylene chloride (dichloromethane, DCM) or a DCM/MMA blend like Weld-On 4 — is applied to a tight-fitting butt joint via capillary action. The solvent dissolves a thin layer on both surfaces, and the polymer chains intermingle as the solvent evaporates, creating a joint that approaches the strength of the parent material (tensile shear strength 20–30 MPa when done correctly).
Requirements for a good solvent joint: edges must be flat and square (surface contact ≥90% across the joint face), gap below 0.05 mm, and the joint face must be free of residual stress. This last point is why laser-cut and machined edges need annealing or mechanical stress relief before solvent bonding — the solvent migrates into stressed material and initiates crazing.
Fixture time: 2–5 minutes for initial set, 24–48 hours for full strength. Do not load the joint before 24 hours.
Structural Adhesive (MMA / Epoxy)
For gap-filling joints, dissimilar material bonding (acrylic to metal or wood), or situations where solvent crazing risk is unacceptable, I use two-part methyl methacrylate (MMA) adhesive (e.g., Scigrip 42 or Plexus MA300). MMA adhesives form a polymer bond without dissolving the substrate surface, which eliminates craze risk. Joint strength is lower than a perfect solvent weld (15–20 MPa shear) but far more tolerant of surface imperfections and gaps up to 1.5 mm.
For bonding acrylic to metals, clear two-part epoxy works but produces a rigid joint with no thermal expansion accommodation. If the assembly will see temperature cycling (outdoor signage, lighting housings), use a flexible MMA adhesive that accommodates the CTE mismatch between acrylic (~70 µm/m·°C) and aluminum (~23 µm/m·°C).
Mechanical Fastening
Screws, rivets, and snap fits are viable but require design accommodations for acrylic’s brittleness. Always use clearance holes (not tapped threads in acrylic), shoulder washers to spread clamping loads, and slotted holes on at least one axis to allow thermal expansion. Never torque a screw directly into acrylic — use a threaded brass or stainless insert (heat-set or press-fit).
| Method | Joint Strength | Gap Tolerance | Craze Risk | Best For |
|---|---|---|---|---|
| Solvent Cement (DCM) | 20–30 MPa shear | <0.05 mm | High if edges stressed | Acrylic-to-acrylic, tight joints |
| MMA Adhesive | 15–20 MPa shear | Up to 1.5 mm | Low | Gap-filling, dissimilar materials |
| Epoxy | 10–15 MPa shear | Up to 2 mm | Very low | Acrylic-to-metal (static assemblies) |
| Mechanical Fasteners | Depends on design | N/A | None | Serviceable joints, thermal cycling |
Shear strength values from Weld-On technical bulletins (IPS Corp.) and Scigrip product datasheets. Tested on cast acrylic butt joints at 23 °C.
6. Surface Finishing
The finishing method determines whether your acrylic part looks like a precision optical component or a rough-cut piece of plastic. Here’s what each method actually delivers in terms of measurable surface roughness.
| Method | Achievable Ra | Edge / Surface | Speed | Limitations |
|---|---|---|---|---|
| Flame Polish (H₂ torch) | Ra <0.05 µm | Edges only | Fast (seconds/edge) | Straight/gently curved edges only; induces surface stress — anneal before solvent bonding |
| Vapor Polish (DCM) | Ra <0.05 µm | Complex surfaces | Medium (1–5 min soak) | Requires fume extraction; slight dimensional change (~0.02 mm); rounds sharp features |
| Mechanical Buff | Ra 0.05–0.2 µm | Large flat faces | Medium | Labor-intensive; risk of heat buildup and local melting if pressure is excessive |
| Wet Sanding (progressive) | Ra 0.2–1.0 µm | Any geometry | Slow | Final grit determines finish; typically 400→800→1500 progression before buffing |
| Diamond Turning | Ra <0.01 µm | Cylindrical / optical | Slow, high cost | Requires diamond-tipped tooling on CNC lathe; for optical-grade lenses only |
Ra values from profilometer measurements on cast acrylic. Flame and vapor polish achieve near-optical clarity; specific Ra below 0.05 µm is below most contact profilometer resolution and measured via white-light interferometry.
For most fabrication projects, the finishing sequence is: rough-sand (180–320 grit) → fine-sand (400–800 grit) → buff with cutting compound → buff with finishing compound. Flame polishing shortcuts this entire sequence for straight edges — a single pass with a hydrogen-oxygen torch melts a micro-layer that re-solidifies glass-smooth. But flame polishing induces surface tensile stress, so treat flame-polished edges the same as laser-cut edges: anneal before solvent bonding.
7. Method Selection Matrix
This is the decision table I keep on the shop wall. Instead of starting with “which machine is available,” start with what the part requires — then the right method picks itself.
| Part Requirement | Recommended Method | Why |
|---|---|---|
| Flat panel, 2D contour, thin sheet (≤12 mm) | CO₂ Laser | Fastest, near-optical edge on cast acrylic, lowest cost per part |
| Flat panel, thick sheet (>12 mm) | Waterjet or CNC router | Laser power insufficient; waterjet gives zero HAZ |
| 3D features (pockets, bores, threads) | CNC milling | Only method for true 3D geometry with tight tolerances |
| Cylindrical / rotational parts (lenses, bushings) | CNC turning | Diamond-tipped tooling produces mirror finish on OD |
| Single-axis bends (brackets, shelves) | Line bending | Simplest forming; minimal tooling cost |
| Compound curves, enclosures, covers | Vacuum / drape forming | Full-sheet forming for organic shapes |
| Straight cuts on thick slabs, rough sizing | Table saw (TCG blade) | Cheapest method; no HAZ; needs secondary finishing |
| Immediate bonding required, no anneal step | Waterjet or saw cut | No thermal stress in cut edge; safe for solvent cement |
| Prototype, 1–5 pieces, complex shape | CNC machining | No tooling investment; digital file → finished part |
| Production, 100+ identical 2D parts | CO₂ laser with nesting | Highest throughput; automated sheet nesting minimizes waste |
8. Defect Troubleshooting Quick Reference
Every defect I’ve seen on the shop floor traces back to one of five root causes: too much heat, residual stress, wrong stock grade, contamination, or wrong tool geometry. Here’s the quick-reference table I hand to new operators.
| Defect | Appears As | Likely Cause | Fix |
|---|---|---|---|
| Crazing | Fine network of micro-cracks, often near edges or joints | Solvent contact on stressed surface (laser-cut, unannealed); or chemical attack (ammonia cleaners) | Anneal edges before bonding (75–80 °C, 2–4 hr); switch to plastic-safe cleaners; use cast stock |
| Melted / gummy edge | Re-welded chips, opaque white or glossy blob on cut face | Feed too slow, RPM too high, dull tool, insufficient chip evacuation | Increase feed rate; reduce RPM; replace tool; add air blast to clear chips |
| Edge chipping | Small fractures along cut edge, jagged profile | Feed too fast, tool not rated for plastics, extruded stock, no back-support | Reduce feed; use O-flute or TCG blade; switch to cast; support exit side of cut |
| Stress whitening (on bend) | White haze line along outer radius of a bend | Bend radius too tight for thickness; sheet under-heated; extruded stock bent across extrusion direction | Increase radius to ≥1.5× thickness (cast) / 2× (extruded); extend heating time; bend extruded along grain |
| Bubbles (thermoforming) | Trapped air pockets in formed part, especially at corners | Sheet overheated; moisture trapped in sheet (common if stored unsealed) | Reduce oven temp by 5–10 °C; pre-dry sheet at 80 °C for 2–4 hr before forming |
| Haze / fogging (vapor polish) | Milky, uneven surface after vapor polishing | Exposure time too long; solvent concentration too high; room humidity above 60% | Reduce exposure time; dilute solvent; control ambient humidity below 50% |
| Joint failure (solvent bond) | Bond separates under light load, chalky white fracture surface | Gap >0.05 mm; contaminated surfaces; edges not flat/square; residual stress in edge | Re-machine edges flat; degrease with IPA; anneal if laser-cut; ensure gap <0.05 mm |
Need Acrylic Parts Fabricated?
Upload your CAD file for a DFM review and quote. CNC, laser, forming — we’ll recommend the right process for your geometry and volume.
Get a Quote →