Urethane Casting Service
Production-quality cast urethane and silicone parts — 1 to 200+ pieces from a single silicone mold, delivered in as fast as 3 days.
Get a Free Quote
Why KUSLA
Your Partner for Urethane & Vacuum Casting
KUSLA's urethane casting service — also known as vacuum casting or polyurethane casting — produces high-quality plastic, rubber, and silicone parts for prototypes and low-volume production. We use 3D-printed or CNC-machined master patterns combined with RTV silicone molds, delivering production-grade results at a fraction of the cost and lead time of injection molding.
Our cast urethane parts closely replicate the mechanical properties, surface finish, and appearance of production thermoplastics — including ABS, polycarbonate, acrylic, and polypropylene. We support insert molding, overmolding, copper EMI shielding, molded-in colors and textures, and custom painting.
Whether you need functional prototypes for design validation, bridge production while hard tooling is being built, or short-run end-use parts, urethane casting gives you the flexibility to iterate quickly and affordably.

Capabilities
Technical Specifications
| Specification | Value |
|---|---|
| Lead Time (First Article) | As fast as 3 days |
| Production Run | 15 business days typical |
| Dimensional Accuracy | ± 0.1 mm (± 0.004 in.), or ± 0.3% on larger dims |
| Shrinkage Rate | + 0.15% typical |
| Maximum Part Size | 914 × 914 × 1829 mm (36 × 36 × 72 in.) |
| Minimum Wall Thickness | 0.75 mm (0.030 in.); 1.5 mm+ recommended |
| Minimum Feature Size | 0.635 mm (0.025 in.) |
| Parts Per Mold | Up to 25 copies (varies by complexity) |
| Surface Finish | Ra 1.6 µm or better (from SLA master) |
Materials
Available Urethane Casting Materials
Polyurethane resins can be formulated to simulate a wide range of production thermoplastics. We organize our materials into three categories to help you select the right match for your application.
| Sub-type | Simulates | Hardness | Color | Reference |
|---|---|---|---|---|
| ABS-Like | General-purpose ABS | Shore D 76–80 | All colors | BJB TC-852 |
| Acrylic-Like | Transparent PMMA | Shore D 80 | Water-clear | Poly-Optic 1410 |
| PC-Like | High-impact PC | Shore D 82–86 | Transparent, USP VI | BJB TC-854 |
| Sub-type | Properties | Hardness | Color | Reference |
|---|---|---|---|---|
| Rubber-Like | High elongation, tear-resistant | Shore A 20–95 | All colors | BJB F-170 |
| Clear Rubber | Colorless, optically clear | Shore A 40–95 | Transparent | BJB WC-565 |
We also cast silicone parts using the same mold process — ideal for medical-grade gaskets, seals, and flexible housings.
Surface Treatment
Finishes for Cast Urethane Parts
Matte
Smooth, non-reflective eggshell texture. Standard finish for functional prototypes.
Glossy
High-shine, mirror-like surface. Ideal for cosmetic models, display housings, and lenses.
Textured
Industry-standard mold textures (MT11010, MT11020, MT11030) for production-like tactile feel.
Custom
Painting (Pantone / RAL match), pad printing, laser engraving, silk screening, soft-touch coating, EMI/RFI shielding.

Urethane Color Options
Polyurethane resins accept pigments at mixing, giving consistent through-color across the entire part. For precise color matching, send us a Pantone number or physical color chip.
Overview
What Is Urethane Casting?
Urethane casting — also called vacuum casting, RTV casting, or polyurethane casting — is a manufacturing process that uses liquid two-part polyurethane resin and flexible silicone molds to produce production-quality plastic or rubber parts. It creates highly precise replicas of a master pattern and is the most cost-effective method for producing 1–200 parts when injection molding tooling is not justified.
How It Works
Urethane Casting Process: 3 Steps
Master Pattern Fabrication
We create the master pattern using high-resolution SLA 3D printing or CNC machining. The master is then hand-finished, sanded, and polished. Every detail — texture, lettering, edge quality — transfers directly to every cast copy.
Silicone Mold Making
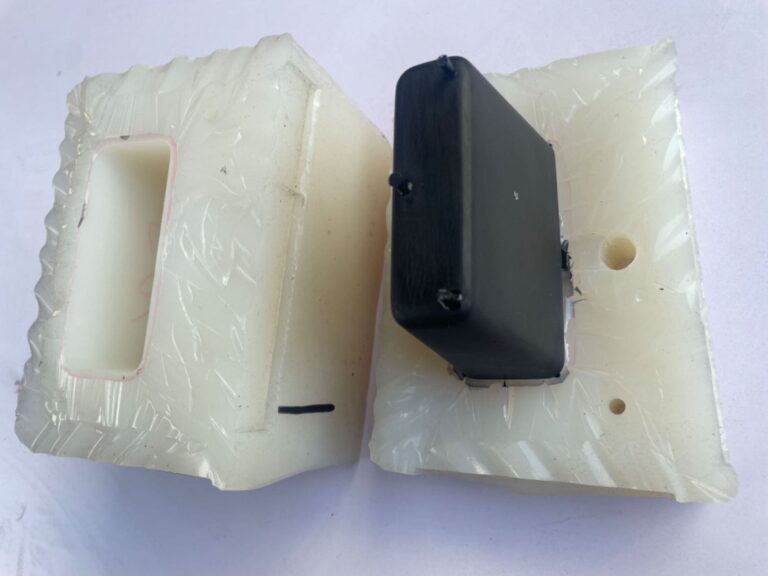
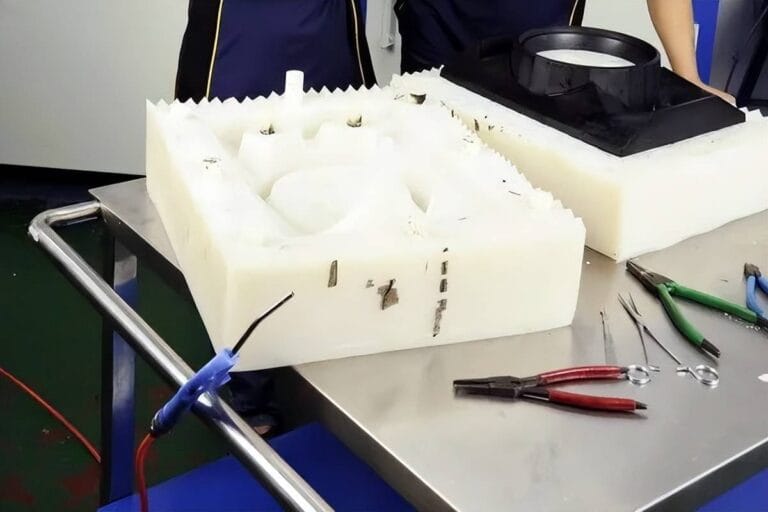
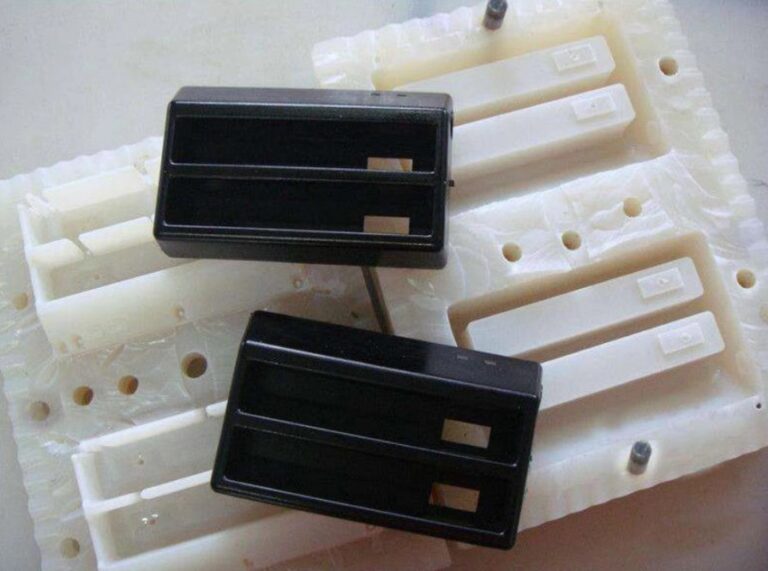
The finished master is suspended in a mold frame, and liquid RTV silicone is poured around it. After the silicone cures (8–16 hours), the mold is precision-cut along a parting line and the master is removed, leaving a flexible two-part mold.
Casting & Curing
Two-part liquid polyurethane resin is mixed and poured into the mold cavity. The mold is placed in a vacuum chamber to remove air bubbles. After curing, the finished part is de-molded. The cycle repeats to produce the required quantity.
Design for Manufacturing
Design Guidelines for Urethane Casting
Following these DFM tips will improve part quality, extend mold life, and reduce cost.
Wall Thickness
Keep walls as uniform as possible to prevent warping and sink marks. Varying thickness is acceptable but should be minimized.
Min 0.75 mm · Recommended 1.5–4 mmDraft Angles
Not required — silicone molds are flexible. But adding draft extends mold life and eases extraction. Essential if transitioning to injection molding later.
Not required · 3–5° recommendedCorner Radii
Use fillets on external corners to improve strength and mold flow. Interior boss corners need smaller fillets to prevent sink marks.
External ≥ 3 mm · Boss ≥ 1.5 mmRibs
Rib thickness should be 40–60% of adjacent wall thickness. Use multiple short ribs rather than one tall rib for best results.
Height ≤ 3× thicknessUndercuts
Freely supported. Flexible silicone molds accommodate complex undercuts, snap-fit features, and internal channels that would require side-actions in injection molding.
No restrictionsTolerances
Standard tolerance for the first 25 mm, plus incremental tolerance per additional 25 mm. Tighter specs achievable with SLA masters.
± 0.25 mm first 25 mm · ± 0.1 mm / 25 mmChoosing the Right Process
Urethane Casting vs. Injection Molding vs. 3D Printing
| Factor | Urethane Casting | Injection Molding | 3D Printing |
|---|---|---|---|
| Tooling Cost | $500–$3,000 | $5,000–$100,000+ | None |
| Lead Time | 3–15 days | 4–8 weeks | 1–5 days |
| Ideal Quantity | 1–200 parts | 500+ parts | 1–10 parts |
| Material | PU simulating production plastics | Actual production thermoplastics | PLA, ABS, Nylon, Resin |
| Surface Finish | Excellent — production-grade | Excellent | Moderate — layer lines visible |
| Mold Life | ~25 shots per mold | 100,000+ shots | N/A |
| Design Changes | Easy — new master pattern | Expensive — mold modification | Easiest — update CAD file |
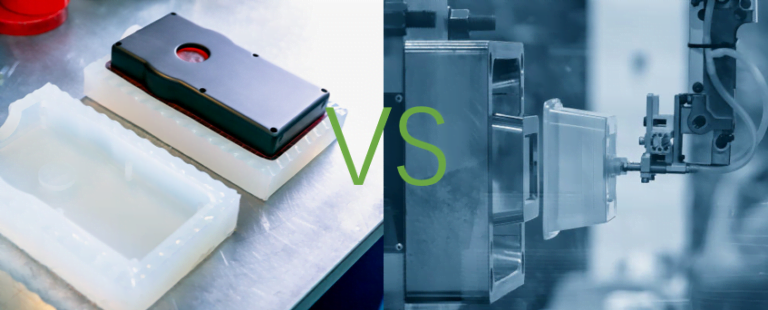
Choose urethane casting when you need fewer than 200 parts, need parts fast, want to validate designs before committing to hard tooling, or require bridge production while injection mold tooling is being manufactured.
Use Cases
Typical Applications
Rapid Prototyping
Functional prototypes ready in 3–5 days for fit, form, and function testing. Ideal for design reviews, investor presentations, and trade shows.
Bridge Production
Produce saleable parts in small batches while injection mold tooling is being manufactured. Seamlessly transition to molded production without design changes.
Consumer & Market Testing
Test different sizes, colors, materials, and textures with real end users before committing to mass production tooling.
Medical Device Housings
USP Class VI biocompatible urethanes for pre-clinical prototypes, surgical tool handles, and wearable device enclosures.
Automotive & Lighting
Clear acrylic-like parts for lens prototypes, light guides, and interior trim evaluation models.
Overmolding & Insert Molding
Combine rigid substrates with flexible elastomer overmolds, or embed threaded inserts, magnets, and PCBs directly into the cast part.
Our Work
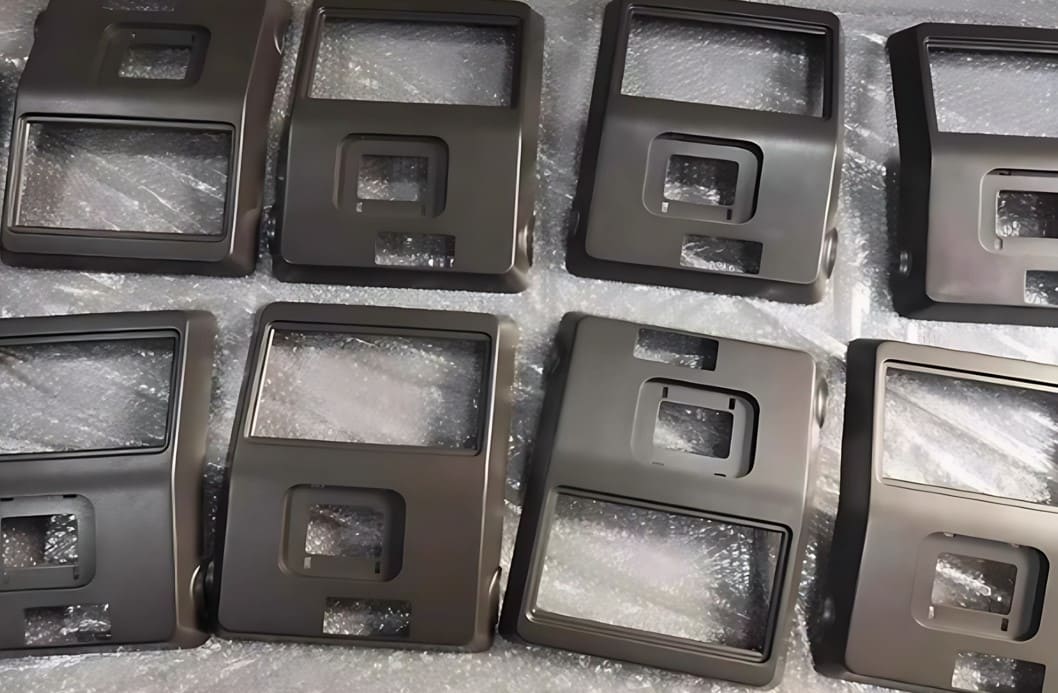
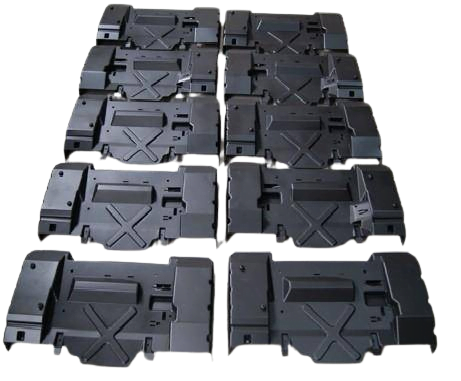
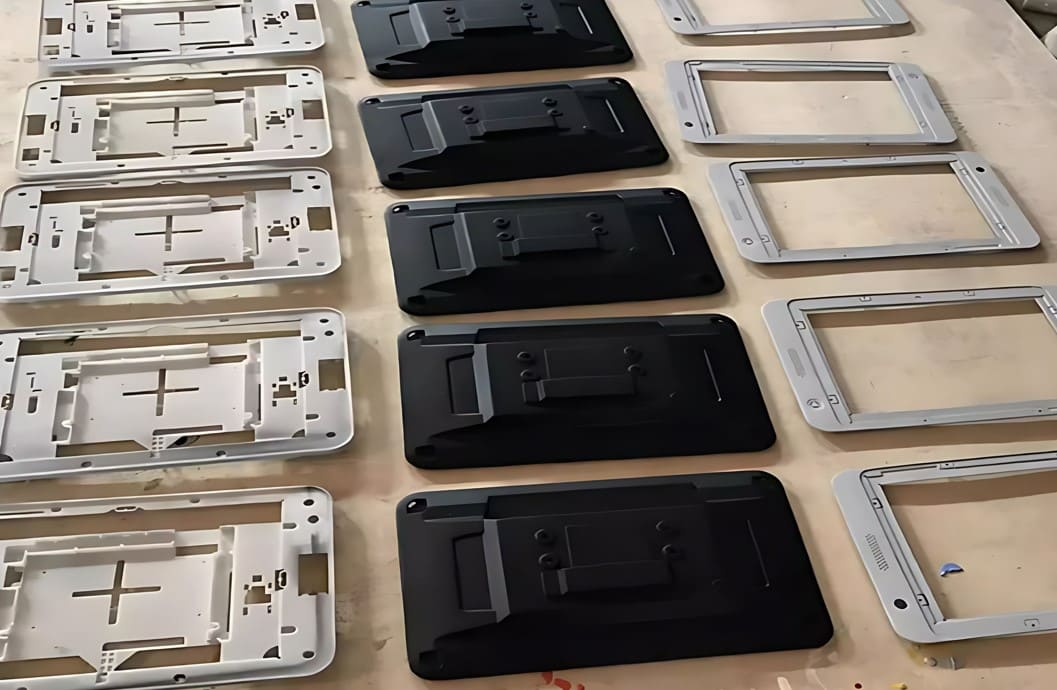
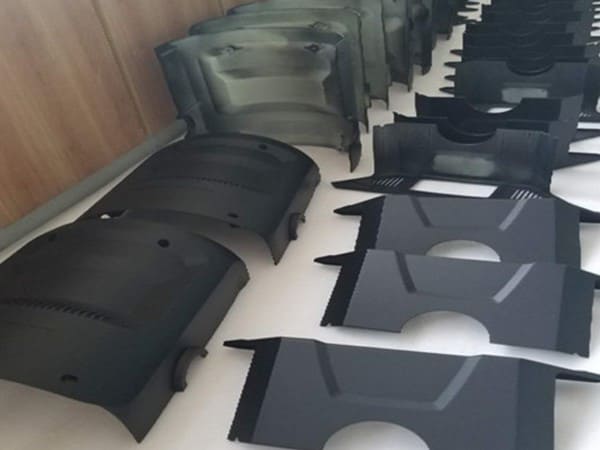
Urethane Parts Gallery

FAQ